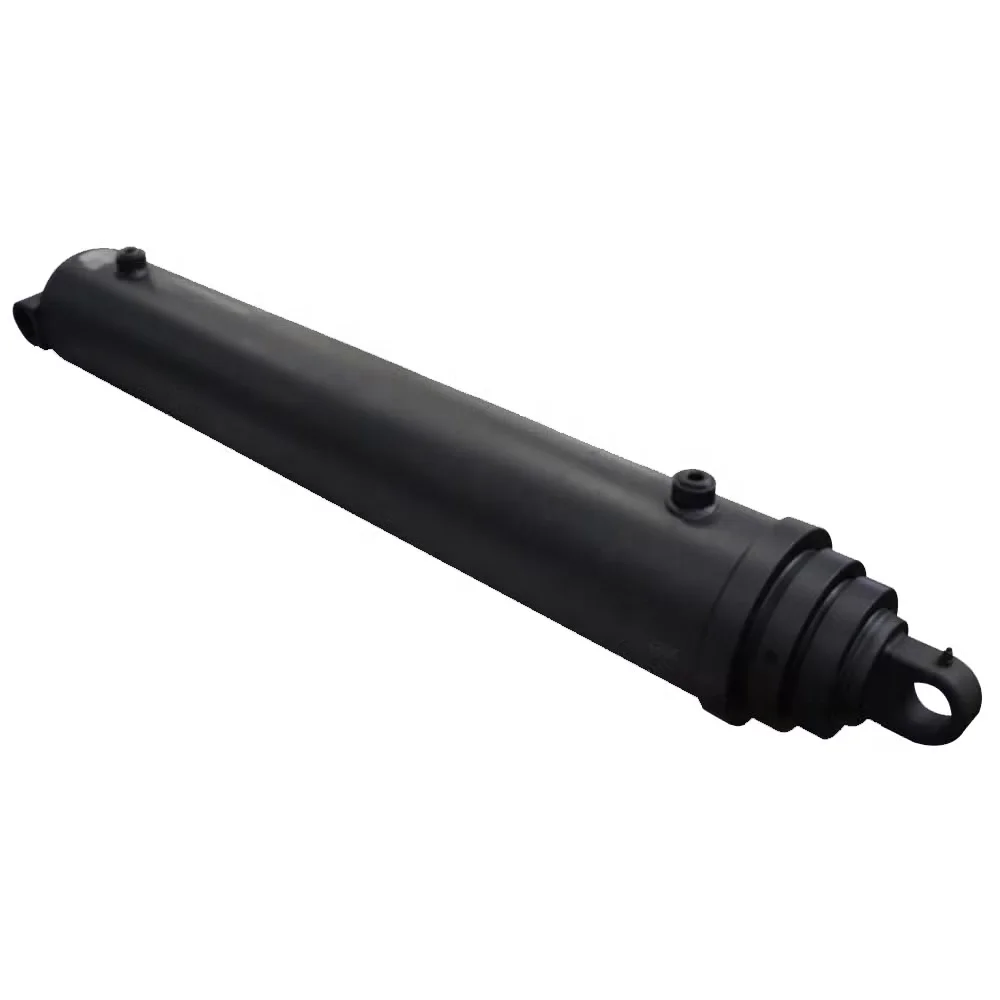

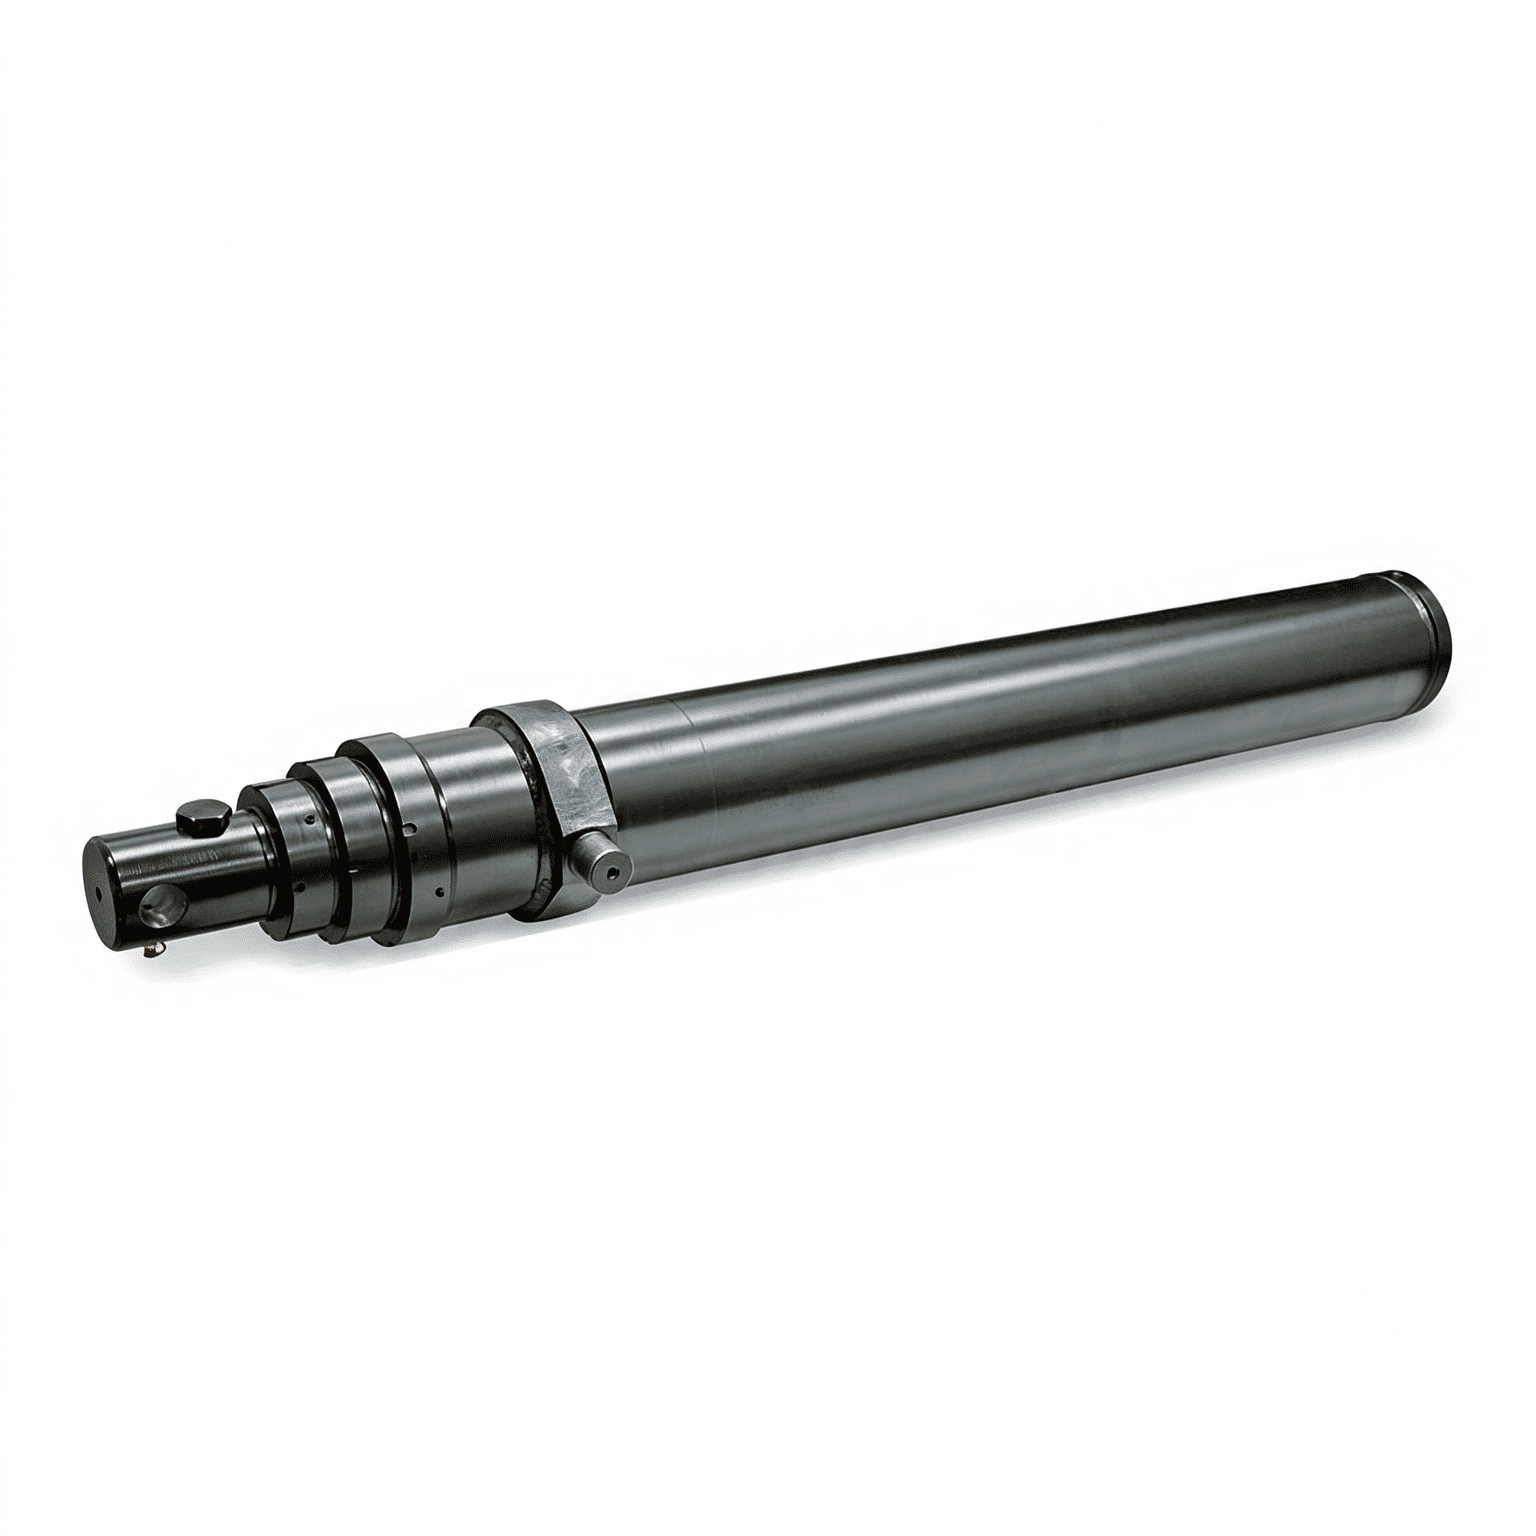
For international equipment manufacturers, fleet rebuilders, and commercial body builders across North America, Europe, Australia, and South America, sourcing custom-engineered hydraulic cylinders from overseas suppliers often comes with four critical operational anxieties:
At HCIC, operating from our headquarters at No. 1177 Chunlan Road in Jinan, Shandong, China, our 36,000-square-meter manufacturing facilities and 20+ senior fluid power design engineers have developed a closed-loop "Blueprint-to-Port" Quality Assurance Protocol specifically engineered to eliminate these procurement risks.
| Parameter | Specification |
|---|---|
| Manufacturing Facility Address | No. 1177 Chunlan Road, Jinan, Shandong, China |
| Workshop & Cleanroom Area | 36,000 Square Meters (3 Facilities + 1 R&D Center) |
| Engineering Design Team | 20+ Experienced Hydraulic Application Engineers |
| CAD / CAE Design Software | SolidWorks, AutoCAD, ANSYS Finite Element Analysis |
| Raw Material Inbound Verification | Direct-Reading Optical Spectrometer & Ultrasonic UT |
| Machining Tolerances & Precision | CNC Lathes & Milling Centers (H8 / f7 Tolerances) |
| Tube Honing & Bore Roughness | Skiving & Roller Burnishing (Ra ≤ 0.2 μm Finish) |
| Piston Rod Hard Chrome Thickness | ≥ 25 μm Micro-Crack-Free Layer (Salt Spray > 500h) |
| End-of-Line Quality Verification | 100% Digital Hydrostatic Proof Test at 1.5x Rating |
| Component Traceability System | Laser-Etched Unique Serial & QR Code Data Matrix |
| Ocean Freight Corrosion Protection | Volatile Corrosion Inhibitor (VCI) Vacuum Barrier |
| Export Crating Standard | Heavy-Duty ISPM 15 Fumigated Plywood Steel Crates |
When an OEM customer submits a 2D PDF, paper blueprint, or sample cylinder, our dedicated engineering team creates a native 3D STEP CAD model within 24 to 48 hours. We perform Finite Element Analysis (FEA) to verify column buckling limits under maximum load, confirm SAE / ISO / BSPP port thread geometry, and verify pin-to-pin installation envelopes.
Before steel is cut, the customer receives a comprehensive General Arrangement (GA) Approval Drawing detailing all critical tolerances (bore H8, rod f7, port thread pitches, pin center-to-center closed lengths, and stroke limits). Full production begins only after signed engineering sign-off.
Every export container from HCIC ships with a complete, digitized Quality Documentation Dossier:
Mill Test Certificates (MTC / EN 10204 3.1): Verifying the exact chemical composition and mechanical yield strength of the steel tubing and rod stock.
First-Article Inspection (FAI) Report: Documenting all critical dimensions measured via digital Coordinate Measuring Machines (CMM) and micrometers.
100% Hydrostatic Pressure Test Certificate: Showing zero-leakage hold data at 1.5 times the rated working pressure (e.g., 30 MPa proof test on a 20 MPa rated cylinder).
Hard Chrome Plating & Salt-Spray Test Report: Certifying micro-crack density and ASTM B117 salt spray corrosion resistance.
| Step | Process |
|---|---|
| 1 | Customer 2D Blueprint / 3D Model |
| 2 | HCIC 24h Engineering Review & FEA Simulation |
| 3 | Customer GA Drawing Approval Sign-Off |
| 4 | Raw Material UT Ultrasonic Testing |
| 5 | Precision CNC Machining & SRB Honing |
| 6 | Cleanroom Assembly & Ultrasonic Wash |
| 7 | 100% Digital 1.5x Hydrostatic Testing |
| 8 | Export VCI Barrier & Steel-Cradled Crating |
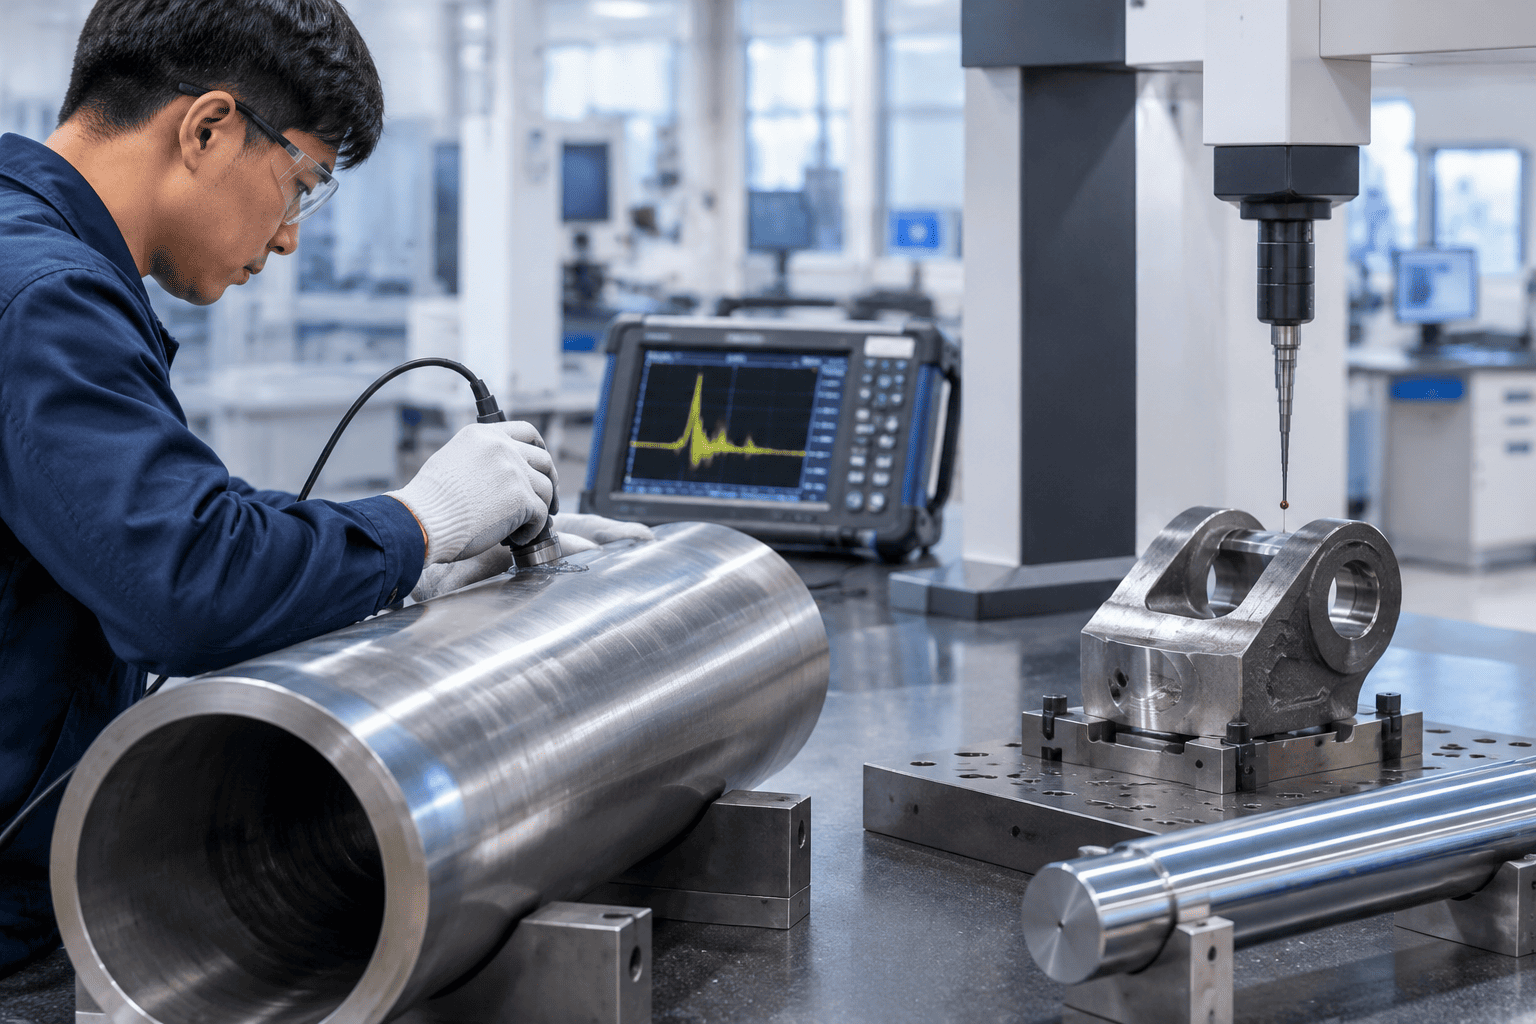
A hydraulic cylinder is only as reliable as the steel beneath its chrome. HCIC enforces strict raw material quality gates before any billet or tube enters the CNC machining queue:
At HCIC, testing is not performed on statistical samples—100% of manufactured cylinders undergo full-pressure testing on computerized digital test benches:
Double-Ended Pressure Proofing: The hydraulic cylinder is mounted horizontally and extended against its internal mechanical stop, with test pressure held at 1.5 times nominal working pressure (e.g., 300 bar for a 200 bar rated cylinder) for a minimum of 3 minutes.
Zero Internal By-Pass Leakage: High-precision digital pressure transducers monitor pressure decay; any drop exceeding 0.2 bar/min triggers an immediate teardown and seal inspection.
Low-Pressure Seal Sensitivity Test: Cylinders are stroked under low pressure (0.5 to 1.0 MPa) to ensure seals do not bind and rod wipers maintain full-circumference contact without stick-slip friction.
Laser QR Code Serialization: Upon passing inspection, the cylinder barrel is laser-etched with a unique serial number and QR code linking directly to its digital inspection log.
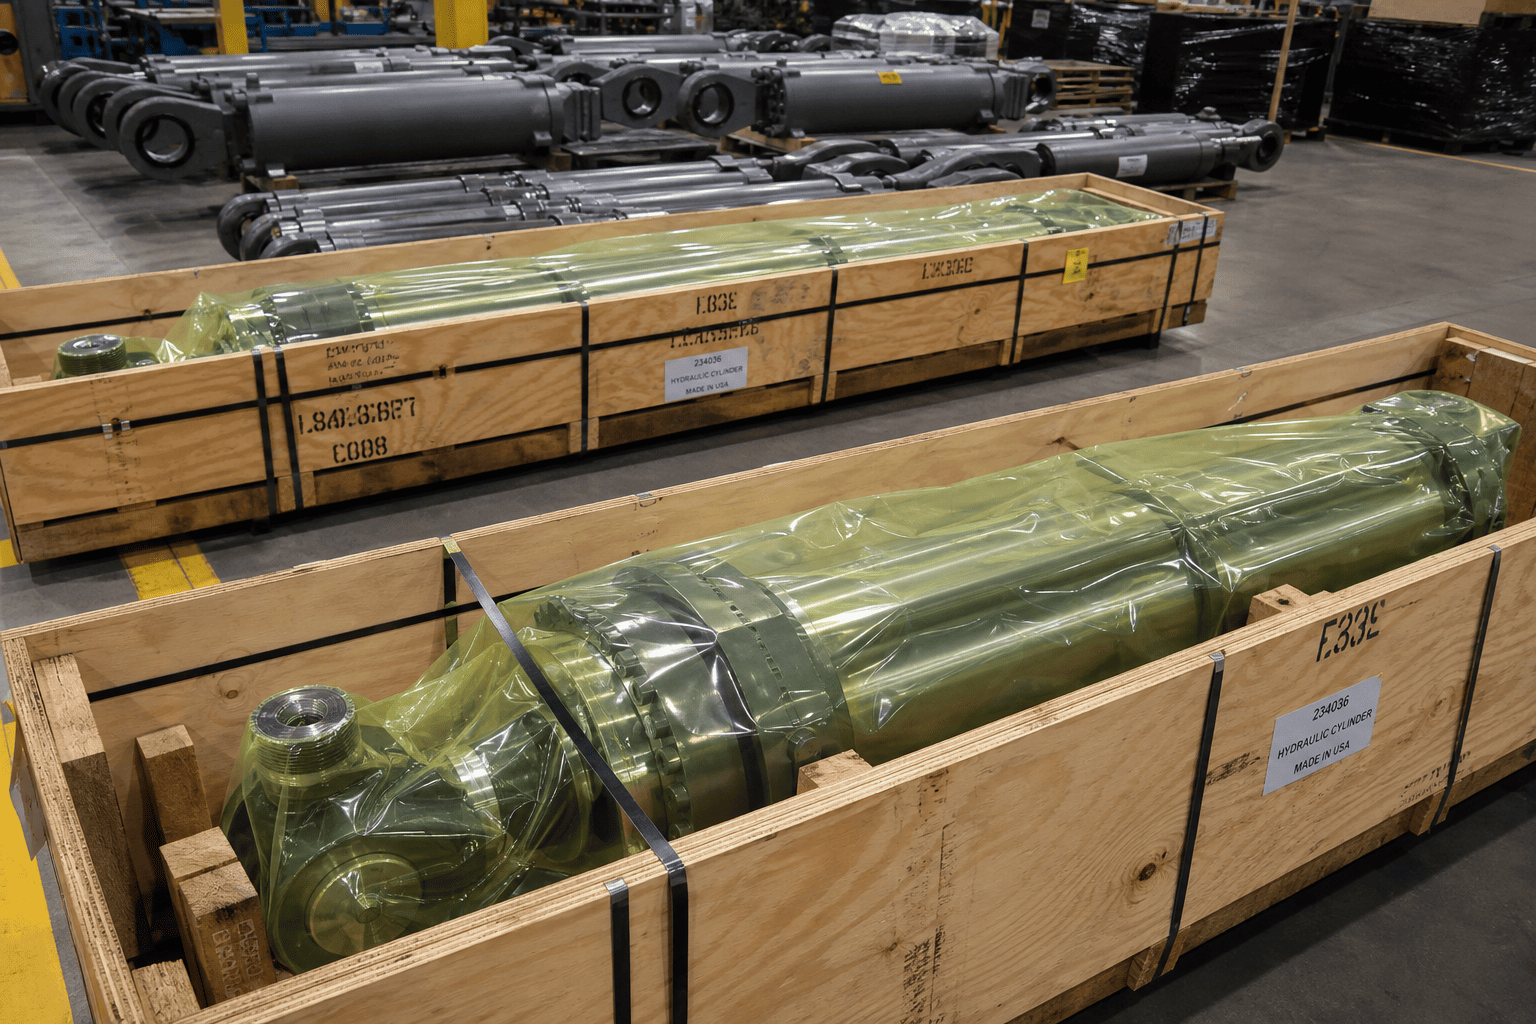
During 30-to-45-day ocean transit through equatorial shipping lanes, salt air condensation inside shipping containers can corrode unprotected metal parts. HCIC implements an industrial 4-Tier Export Preservation Standard:
| Tier | Description |
|---|---|
| Tier 1 | Internal Corrosion Inhibitor: Cylinders are filled with calibrated testing oil infused with anti-corrosion additives, and ports are sealed with threaded caps. |
| Tier 2 | External Protective Wax: Hard-chrome rods and bare metal pin eyes receive a heavy-duty, marine-grade protective rust-preventative wax coating. |
| Tier 3 | VCI Sealed Enclosure: Each individual cylinder is sealed inside a thick Volatile Corrosion Inhibitor (VCI) barrier bag that emits rust-inhibiting ions. |
| Tier 4 | Heavy Plywood Crating: Packed in ISPM 15 fumigated solid plywood cases with internal custom-notched steel support cradles and high-tensile steel banding. |
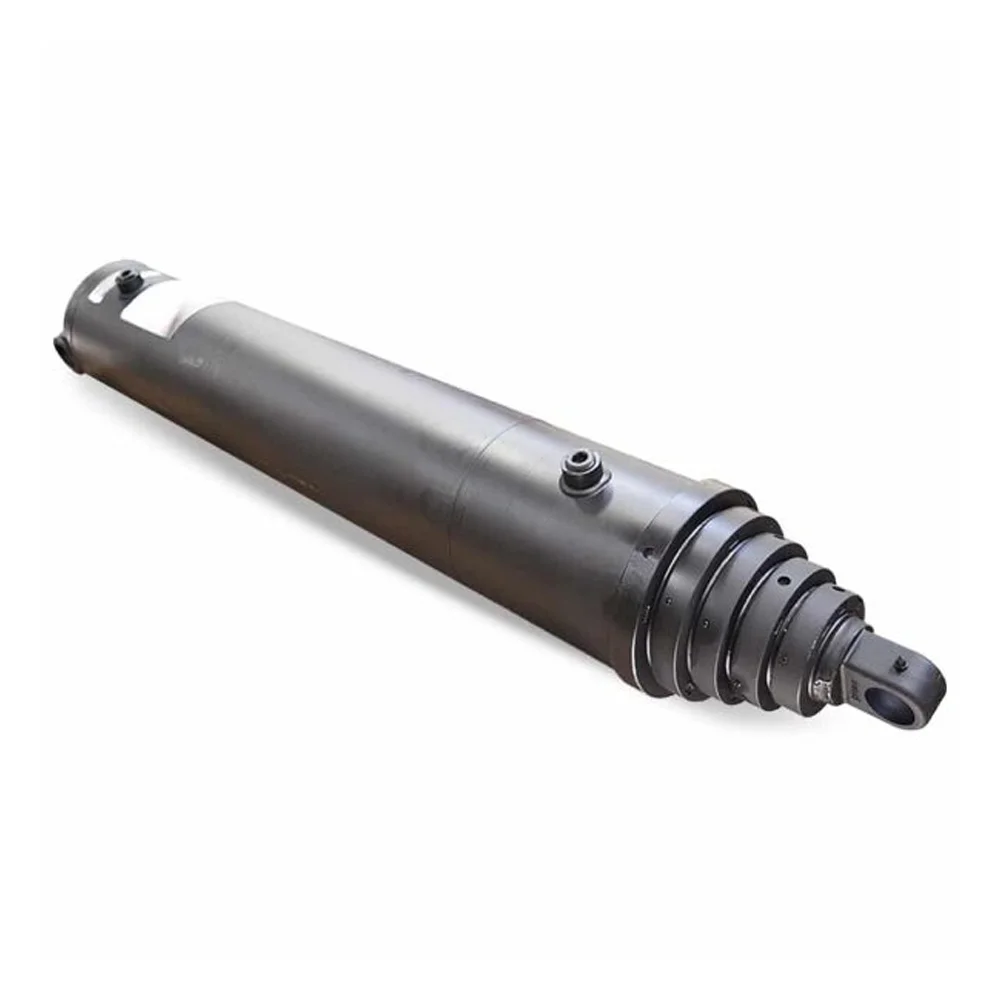
Whether you require a standard 5-stage telescopic dump hoist, a double-acting refuse packer ram, or a custom smart cylinder with embedded linear sensors, HCIC’s engineering and manufacturing infrastructure is built to support your growth.
Whether you require a standard 5-stage telescopic dump hoist, a double-acting refuse packer ram, or a custom smart cylinder with embedded linear sensors, HCIC’s engineering and manufacturing infrastructure is built to support your growth.